Project Overview
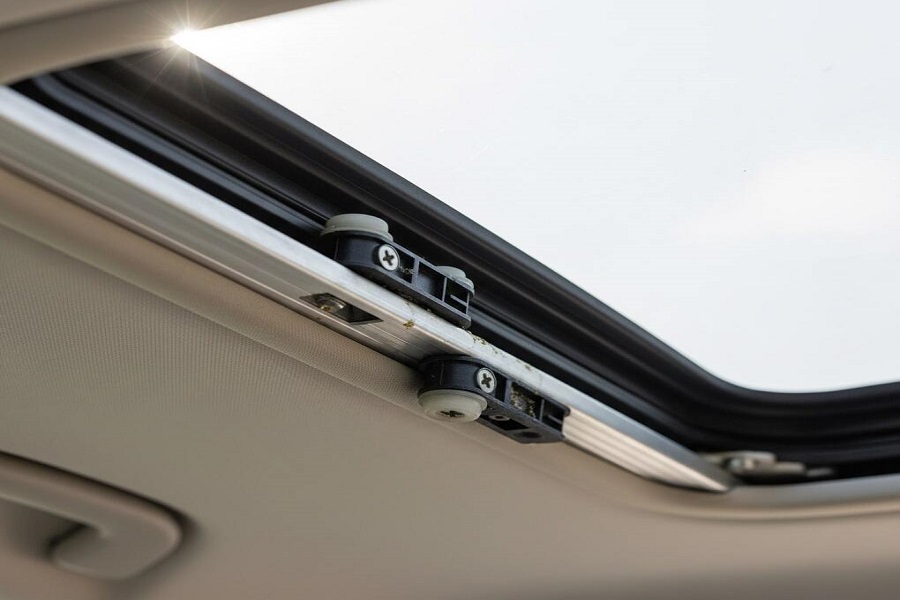
The project involved modifying an existing Special Purpose Machine (SPM) to improve the machining process for an aluminium extrusion component. The original SPM concept had two drilling heads mounted at the top, but the project was discontinued before the machine could be implemented. The vendor subsequently required a revised arrangement with side drilling, counterboring and tapping operations. Enginerio was engaged to redesign the relevant machine assemblies and develop a suitable production fixture.
Initial Manufacturing Challenge
The component had previously been processed using a punching press. This approach was suitable for limited quantities, but production output was low and the process was not ideal for the required repeatable machining operations. The component required machining at defined lengths and locations, including three different hole features. The revised process needed to accommodate drilling from both the top and the side, together with tapping.
SPM Redesign and Machine Modification
The existing machine was assessed using dimensions taken manually from the SPM. Based on the available measurements and the vendor’s revised requirements, the drill-head mounting arrangement was redesigned.
- Reconfigured the drilling arrangement to accommodate a side-mounted drilling head.
- Modified the top drilling head to include a counterbore drilling operation.
- Provided tapping capability for both the top and side drilling arrangements.
- Designed new drill-head mounting structures and integrated a tapping-head mount sourced from another SPM.
- Coordinated the revised layout so the required machining operations could be performed on the component.
The redesign focused on adapting the existing machine rather than developing a completely new SPM, helping the vendor reuse available equipment and reduce the need for a full machine replacement.
Nylon Fixture Development
A dedicated nylon fixture was designed for machining on a VMC. Nylon was selected to support the aluminium extrusion without marking or damaging its mill-finish surface. The component was supplied without anodising, so avoiding scratches, dents and surface impressions was particularly important.
To control fixture cost, an initial continuous nylon fixture approximately 4 metres long was developed. During production trials, however, the natural bend and twist variation in the extruded aluminium caused uneven loading against the long nylon support. This led to wear and damage to the nylon fixture after a short period of use.
Fixture Improvement: Stainless-Steel Support Jigs
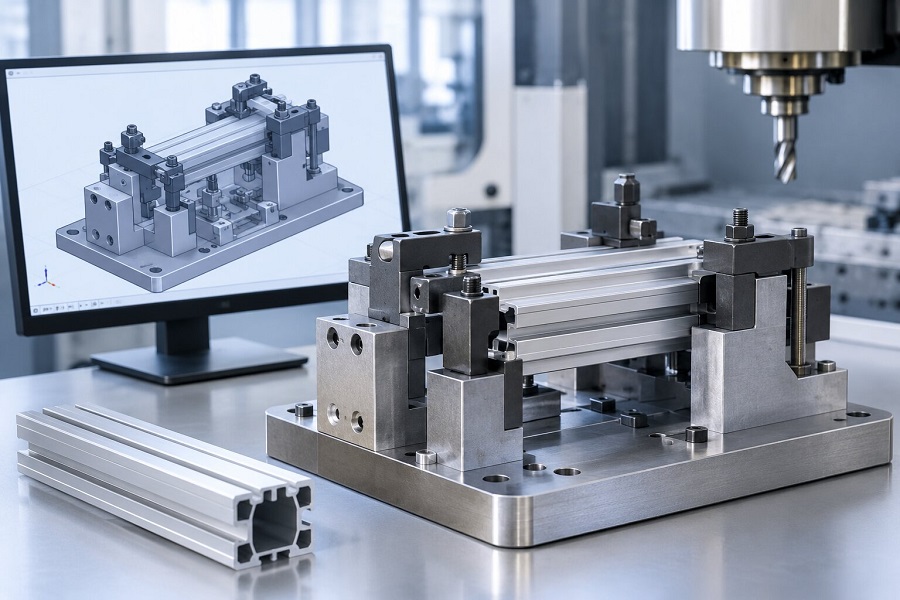
The fixture was reviewed to address the wear issue without compromising protection of the extrusion surface. Stainless-steel support jigs were introduced at the starting, middle and end support locations. These support points improved the stability of the long extrusion and reduced the load and stress concentrated on the nylon fixture.
The revised arrangement retained the nylon contact/support surfaces where needed to protect the mill-finish aluminium, while the stainless-steel jigs provided stronger and more durable support at key locations. This resolved the recurring fixture-damage issue and extended fixture service life.
Execution and Timeline
The SPM redesign and production-fixture development were completed within one week. The work included manual measurement of the existing machine, redesign of the drill-head mounts, integration of the tapping mount, nylon fixture design for VMC machining, and the subsequent support-jig improvement.
Results and Benefits
- Converted a low-output punching-press process into an SPM-based machining approach.
- Enabled the required top and side drilling operations, including counterboring and tapping.
- Reused the existing SPM structure and an available tapping-head arrangement instead of starting from a completely new machine design.
- Developed a fixture solution that protected the aluminium extrusion’s mill-finish surface.
- Addressed fixture damage caused by extrusion bend and twist by adding stainless-steel support jigs at key locations.
- Improved fixture durability and reduced the need for frequent nylon-fixture replacement.
- Completed the design and production-fixture development in one week.
Engineering Value Delivered
This project demonstrates a practical approach to machine retrofitting, rapid mechanical design and production fixture development. By measuring and adapting existing equipment, integrating additional machining functions, and improving the fixture based on actual production behaviour, the team delivered a workable solution within a short timeline. The final design balanced production requirements, surface protection, fixture durability and cost.
Project Capabilities Demonstrated
SPM modification and retrofitting | Drill-head and tapping-mount design | Manual machine measurement | VMC fixture design | Aluminium extrusion machining support | Nylon and stainless-steel fixture integration | Design-for-manufacturing | Rapid project execution